Premium Stripped Walnut Kernels and Walnut 1 4 kg Price Guide
For professional procurement managers in the confectionery and baking industries, sourcing high-quality stripped walnut kernels requires a balance between precise technical specifications and cost-efficiency. Whether you are evaluating the walnut 1 4 kg price for retail packaging or sourcing bulk tonnage for industrial production, the integrity of the kernel and the stability of the supply chain are paramount. High-grade kernels, particularly Extra Light Halves, are essential for premium products where visual appeal and a clean, non-bitter taste profile are non-negotiable.
Hebei Luhua Import and Export Trade Co., Ltd. bridges the gap between raw agricultural output and industrial requirements. By integrating a 30,000 mu planting base with advanced BRC-certified processing facilities, we provide stripped walnut kernels that meet rigorous international food safety standards. From low-temperature roasting to high-precision X-ray impurity removal, our process ensures that every batch maintains its nutritional density and optimal color grading, providing a reliable foundation for global food manufacturers.

Industrial Processing Standards for Premium Stripped Walnut Kernels
The quality of a stripped walnut kernel is determined long before it reaches the packaging stage. At our facilities, we employ a multi-stage purification process designed to eliminate the bitterness associated with the outer skin while preserving the delicate oils of the nut. Unlike traditional chemical stripping, our physical removal process ensures a natural flavor profile, making the kernels ideal for high-end baked goods and health-conscious snacks.
To maintain absolute purity, we utilize a sophisticated sequence of separation technologies. Air separation removes lightweight debris, while high-precision color separators grade the kernels into specific categories such as Extra Light, Light, and Amber. To guarantee the absence of malignant impurities, we implement professional X-ray separation equipment—a critical step for BRC-certified operations that ensures the product is safe for international export to markets in Europe and Southeast Asia.
- Physical Skin Removal: Eliminates bitterness without compromising nutritional value.
- Low-Temperature Roasting: Enhances sweetness and retains essential omega-3 fatty acids.
- Multi-Stage Sorting: Integration of infrared and X-ray technology for zero-defect quality control.
- Cold Storage Stability: 1,000-ton capacity ensures freshness and consistent supply regardless of harvest cycles.

Analyzing Grade Specifications: From Extra Light Halves to Mixed Crumbs
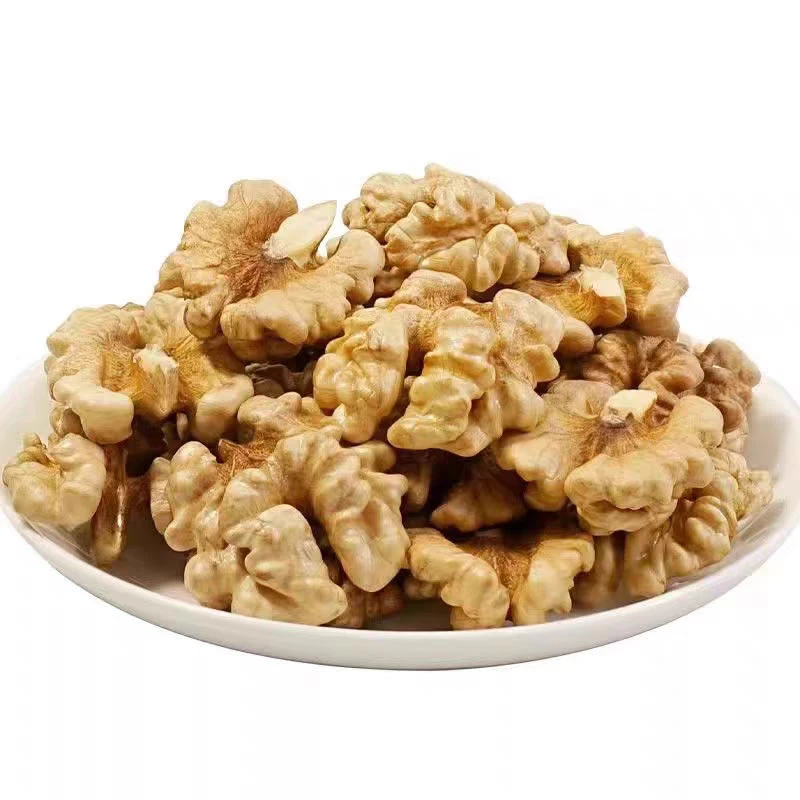
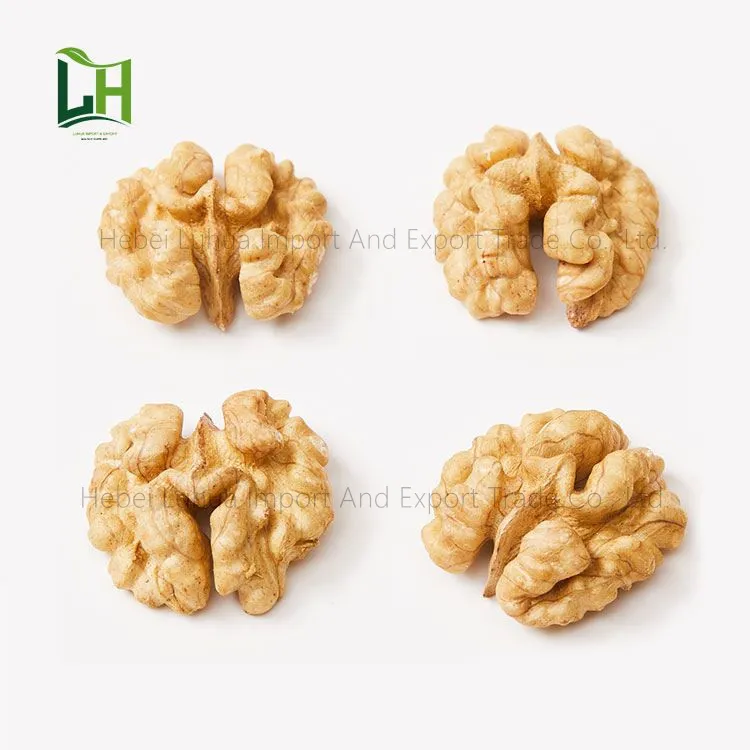
In the global walnut trade, grading is the primary driver of value and application. The "Light" color spectrum is highly prized in the Western market for its aesthetic appeal in cakes and salads. Extra Light Halves (ELH) represent the pinnacle of quality, characterized by high integrity (minimal breakage) and a pale, uniform color. These are typically reserved for luxury confectionery where the whole half-kernel is a visual requirement.
For industrial baking, such as bread or granola production, Light Quarters (LQ) or Light Pieces (LP) offer a more cost-effective solution without sacrificing the flavor profile. The transition from "Light" to "Amber" signifies a deeper natural hue; while Amber kernels are equally nutritious, they are often utilized in darker doughs or processed nut butters. Understanding these distinctions allows procurement officers to optimize their cost-per-unit based on the final product's visual and structural needs.
Our production lines are capable of delivering any of these specifications with high consistency. By maintaining a daily output of up to 50 tons and leveraging a large-scale cold storage system, we prevent the oxidative rancidity that often plagues smaller suppliers, ensuring that the color and taste remain stable from the factory floor to the end consumer.
Strategic Procurement: Balancing Quality, Volume, and Delivery Logistics
Procuring walnuts at scale involves managing risks related to crop volatility and logistics delays. A common challenge for wholesalers is maintaining sufficient inventory without risking spoilage. Our integration of industry and trade allows us to control the process from the 30,000 mu planting base to the final vacuum-sealed package. This vertical integration reduces the number of intermediaries, thereby stabilizing the price and ensuring a faster delivery window, typically between 7 to 15 days.
Packaging is another critical variable in maintaining product shelf life. We offer flexible options, including 10kg and 12.5kg bulk bags, as well as 2x5kg vacuum packaging to prevent oxygen exposure. For clients requiring OEM or ODM services, we provide customized labeling and packaging to meet specific retail or regional regulatory requirements. This flexibility is essential for distributors who need to move products quickly from the port to the retail shelf.
When evaluating potential suppliers, buyers should look beyond the initial quote. The presence of BRC certification, the capacity for year-round stock, and the use of X-ray separation are indicators of a supplier's ability to handle large-scale, high-risk food contracts. Our experience exporting to over 100 countries has taught us that reliability in delivery and consistency in grading are the most valued assets in a long-term partnership.
Walnut Kernel Grading and Application Matrix
| Grade Specification | Color Profile | Physical Integrity | Primary Application |
|---|---|---|---|
| Extra Light Halves (ELH) | Pale/Creamy | High (Whole Halves) | Premium Confectionery / Garnish |
| Light Halves (LH) | Light Gold | High (Whole Halves) | High-end Bakery / Retail Packs |
| Light Quarters (LQ) | Light Gold | Medium (1/4 pieces) | Granola / Mixed Nut Blends |
| Light Pieces (LP) | Light Gold | Low (Broken) | Industrial Cake Fillings / Bases |
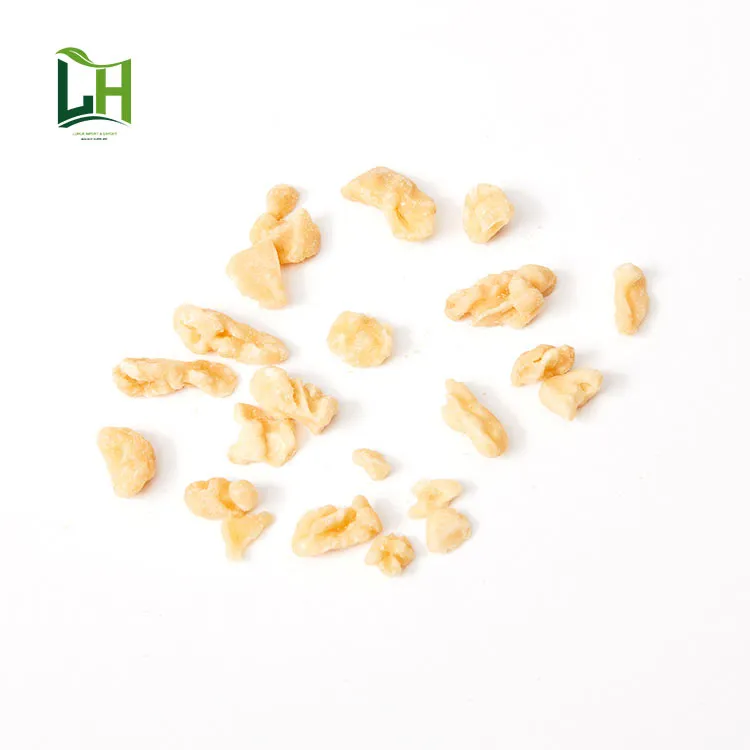
| Amber Mixed Crumbs | Deep Gold/Brown | Very Low (Smallest) | Nut Butters / Oil Extraction |
Optimizing Nutritional Value through Low-Temperature Processing
The nutritional integrity of walnuts, particularly their omega-3 fatty acids and antioxidants, is highly sensitive to heat. Standard high-temperature roasting can lead to the degradation of these healthy fats and the development of an acrid taste. To counter this, Hebei Luhua utilizes low-temperature roasting technology. This method ensures the walnut kernels are fully ripe and aromatic while preserving the natural sweetness and medicinal properties of the nut.
From a health perspective, the timing of consumption can vary based on user needs. In the morning, the protein and healthy fats provide a sustained energy release, supporting cognitive function throughout the workday. Conversely, the natural melatonin content in walnuts makes them a beneficial evening snack to support relaxation and sleep quality. By providing a clean, stripped product, we make these nutritional benefits more accessible for a wide range of consumer applications.
Furthermore, the choice between shelled and in-shell walnuts is a matter of logistics versus longevity. While in-shell walnuts offer a natural protective barrier, our vacuum-packed stripped kernels provide the convenience required for modern industrial food production. Through strict temperature control and BRC-certified hygiene standards, we extend the shelf life of our shelled kernels up to 24 months, matching the efficiency needed for global distribution.
Future Trends in Global Walnut Sourcing and Quality Management
The global nut industry is shifting toward total traceability and "clean label" production. Buyers are increasingly demanding transparency regarding the origin of the crop and the methods used for skin removal. The move toward integrated industry-trade models, where the processor also manages the planting base, is becoming the standard for ensuring sustainable quality and ethical sourcing. This trend reduces the risk of contamination and ensures that the product meets the evolving food safety laws of the EU and North America.
Technological advancements in sorting are also redefining "quality." The adoption of AI-driven color sorting and X-ray detection allows for a level of precision that was previously impossible. For the procurement manager, this means a reduction in waste and a guarantee that the specifications ordered are exactly what is delivered. As the market for healthy, plant-based proteins grows, the demand for high-integrity, light-colored walnut kernels is expected to rise, particularly in the functional food sector.
For those seeking a stable partner, the focus should remain on suppliers who invest in both agricultural infrastructure and processing technology. By combining a 30,000 mu base with advanced BRC-certified factories in Xinjiang, Hebei, and Yunnan, we are positioned to meet this evolving demand, providing a scalable solution for businesses looking to expand their global footprint in the healthy snacks and baking ingredients market.
Frequently Asked Questions Regarding Walnut Kernel Procurement
What is the difference between Light and Amber walnut kernels?
The difference is primarily visual. Light kernels have a pale, creamy color and are generally more prized for premium retail and high-end bakery products. Amber kernels have a deeper golden-brown hue; they are nutritionally identical to light kernels but are often used in products where a darker color is acceptable or desired, such as in nut butters or certain types of bread.
How does BRC certification benefit the end buyer?
BRC (British Retail Consortium) certification is a globally recognized standard for food safety. For the buyer, it provides an independent guarantee that the factory follows strict hygiene, quality control, and safety protocols. This reduces the risk of contamination and ensures the product is compliant with the stringent import regulations of most developed countries.
Can you provide customized packaging for OEM orders?
Yes, we provide comprehensive OEM/ODM services. This includes customized label design and packaging specifications. We offer standard options like 10kg, 12.5kg, and 2x5kg vacuum packs, but we can adjust these based on your specific market requirements and retail needs.
What is the typical shelf life of stripped walnut kernels?
Our stripped walnut kernels have a shelf life of up to 24 months when stored under proper conditions. To maximize freshness, we recommend storing them in airtight containers in a cool, dry environment, or preferably in a refrigerator or freezer to prevent the natural oils from oxidizing.
How do you ensure the walnut kernels are free from impurities?
We use a comprehensive, multi-stage cleaning process. This includes air separation for light debris, high-precision color sorting for grading, infrared light separation for fine impurities, and professional X-ray equipment to detect and remove malignant impurities that are invisible to the naked eye.
What is the typical delivery time for international shipments?
Our standard delivery time is between 7 to 15 days. Because we maintain a 1,000-ton cold storage facility and have our own production lines, we can achieve faster turnaround times and ensure a stable supply throughout the year, regardless of the harvest season.
Industry Resources and Technical References
- BRC Global Standards for Food Safety
- Food and Agriculture Organization of the United Nations
- U.S. Food and Drug Administration - Nut Safety Guidelines
- European Food Safety Authority
Whether you are managing a large-scale industrial bakery or a specialty nut distribution network, the quality of your raw materials defines your final product. Hebei Luhua is committed to providing the consistency, certification, and scale necessary to support your business growth. Contact us today to discuss your specific grading requirements and receive a detailed quotation tailored to your volume needs.
Related Industry Insights